A practical breakdown of what goes into concrete — cement types, aggregates, water-cement ratios, and admixtures — and how each ingredient affects the final strength and workability of your mix.
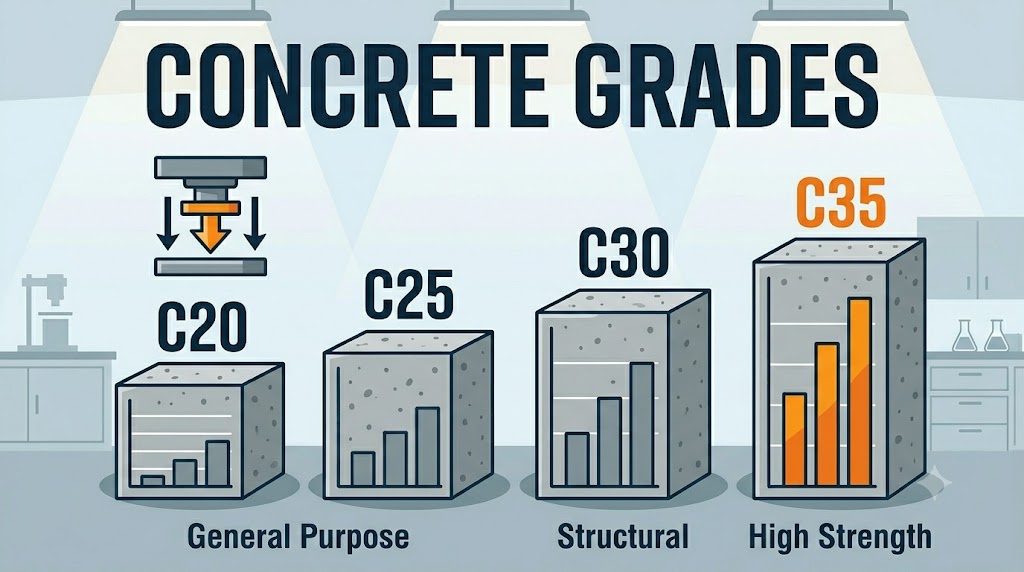
C-grades — C20, C25, C30, C35, and upward — are characteristic compressive strength classes defined by Eurocode 2 (EN 206) and used across the UK, Europe, and Commonwealth countries. The number is the cylinder strength in MPa, measured at 28 days on a 150 mm × 300 mm cylinder test specimen. C30 means 95% of cylinders tested will exceed 30 MPa (4,350 PSI). Every structural concrete element on a Eurocode-designed project has a minimum C-grade specification; using the wrong one is a code violation.
What C-grade notation actually specifies
EN 206 expresses grades as C(cylinder)/cube — so C30/37 means a characteristic cylinder strength of 30 MPa and a characteristic cube strength of 37 MPa. Cylinder results run approximately 80% of cube results for the same mix, which is why the two numbers differ. UK practice historically used cube testing (BS 5328), and many contractors still think in cube terms; the cube strength is the higher of the two numbers in the designation.
The concrete compressive strength converter converts between cylinder MPa, cube MPa, and PSI — essential when comparing a UK spec (cube) against a Eurocode spec (cylinder) or a US readymix plant’s PSI rating.
The C-grade defines a statistical floor, not an average. The target mean strength used by the ready-mix plant to design the actual mix is higher than the specified grade, to account for production variability. For C30 with a production standard deviation of 5 MPa, the target mean strength is 30 + (1.645 × 5) = 38.2 MPa. This is why delivered concrete routinely test higher than the C-grade — that is intentional and correct.
C20 to C50: grades, equivalent PSI, and structural applications
Grade (EN 206)
Cylinder (MPa)
Cube (MPa)
PSI (approx.)
Structural application
C16/20
16
20
2,320
Blinding, mass fill, non-structural slabs
C20/25
20
25
2,900
Foundations, ground slabs, lightly loaded elements
C25/30
25
30
3,625
Residential RC slabs, beams, columns
C28/35
28
35
4,060
Commercial floors, heavier foundations
C30/37
30
37
4,350
Bridges, parking structures, retaining walls
C32/40
32
40
4,640
Heavily loaded structures, water retaining
C35/45
35
45
5,075
Prestressed elements, marine structures
C40/50
40
50
5,800
High-rise columns, pre-cast beams
C45/55
45
55
6,525
Offshore, bridge decks, industrial floors
C50/60
50
60
7,250
High-performance structural members
For residential work in the UK, the most common grade on a structural engineer’s drawing is C25/30 for ground-bearing slabs, pad foundations, and domestic RC frames. C30/37 appears in commercial basements, retaining walls, and any element with significant reinforcement. Below C20/25, concrete is considered non-structural and should only be used as blinding or mass fill.
How C-grades relate to exposure classes under EN 206
EN 206 ties minimum concrete grade to exposure class. The designation covers chemical and physical attack: XC (carbonation), XD (chloride from non-seawater), XS (chloride from seawater), XF (freeze-thaw), XA (chemical attack). For each class there is a minimum grade, a maximum w/c ratio, and a minimum cement content. Note that EN 206 is a framework standard — individual countries set the exact numeric limits through their National Annex (BS 8500 in the UK, DIN in Germany, and so on), so figures below are representative of common UK/BS 8500 practice rather than a single universal number; confirm against your specific national annex before finalising a spec.
Exposure class
Description
Min grade (EN 206)
Max w/c
XC1
Dry or permanently wet
C20/25
0.65
XC2
Wet, rarely dry
C25/30
0.60
XC3/XC4
Moderate/cyclic wet-dry
C30/37
0.55
XD1
Chloride, moderate humidity
C30/37
0.55
XD2/XD3
Chloride, wet or cyclic
C35/45
0.45
XS1
Marine, airborne salt
C30/37
0.50
XS2/XS3
Submerged / tidal
C35/45
0.45
XF1–XF4
Freeze-thaw (four sub-classes of increasing severity — this range spans all four, not one figure per class)
C25/30–C30/37
0.45–0.55
A basement retaining wall in a UK car park with deicing salts (XD3 exposure) requires a minimum of C35/45 with a maximum w/c of 0.45 and a minimum cement content of 360 kg/m³. Specifying C30/37 in that environment is non-compliant regardless of whether it is structurally adequate — durability and strength requirements must both be met, and the more demanding criterion governs.
Common mistakes when specifying or ordering C-grade concrete
Specifying the cylinder strength when the plant expects cube. In the UK, most ready-mix plants still quote and batch to cube strength. If you order ‘C30 concrete’ without specifying cylinder or cube, you may receive concrete designed to C30 cube (37 MPa cylinder) when your engineer specified C30 cylinder (37 MPa cube). Always use the full EN 206 designation — C30/37 — and confirm with your plant which test method they use for compliance.
Using C20/25 for exposed concrete in freeze-thaw climates. C20/25 has insufficient density and cement content to resist freeze-thaw cycling. In Scotland, Northern Ireland, or anywhere with more than 25 freeze-thaw cycles per year, the minimum for exposed slabs, paths, and driveways is C25/30 with air entrainment (3–6% entrained air). C20/25 without air entrainment will surface-scale within 3–5 winters.
Ordering standard C-grade concrete for sulphate-bearing ground. Sites with ground sulphate content above Class DS-2 (SO₃ > 0.5 g/L in groundwater) require sulphate-resisting Portland cement (SRPC) or a specified blend with GGBS. The C-grade alone does not address this — you can have C40 concrete that deteriorates in sulphate ground if the cement type is wrong. Always check the site investigation report for sulphate classification before specifying foundations.
Assuming higher C-grade always means better concrete for the application. C50/60 in a domestic house foundation is money wasted and potentially problematic — higher-grade concrete is stiffer (higher modulus), more prone to early thermal cracking in thick sections, and requires tighter placing and curing procedures that site crews are not set up to follow. Specify the minimum grade that satisfies both structural and durability requirements.
Related calculators you might need
Knowing the C-grade is the first step; calculating the volume of concrete you need is the next. For foundations, the concrete footing calculator outputs m³ for pad and strip footings at any dimension. For ground-bearing slabs, the concrete slab calculator handles rectangular and irregular areas. Once you have a volume, the concrete cost calculator can apply your local ready-mix price to get a delivered cost. If the project uses high-grade concrete (C35+) and you need to verify load-bearing capacity, the concrete load capacity calculator is the relevant structural check.
Frequently asked questions
What is C25 concrete used for?
C25/30 is the most common grade for residential reinforced concrete in the UK — used for house foundations, ground floor slabs, garden walls, retaining walls up to about 1.5 m / 5 ft, and lightly loaded beams and columns. It has a 28-day cylinder strength of 25 MPa (3,625 PSI) and cube strength of 30 MPa. It is the minimum grade most structural engineers specify for any load-bearing reinforced concrete member.
What is the difference between C30 and C35 concrete?
C30/37 has a characteristic cylinder strength of 30 MPa; C35/45 has 35 MPa — a 17% increase in strength. C35/45 also requires a lower maximum w/c (0.45 vs 0.50 for XC4) and higher cement content. In practice, C35 is specified for more aggressive exposure conditions — parking structures, bridge decks, retaining walls in chloride environments — rather than simply for load capacity. The ready-mix cost difference is typically £8–£18 / $12–$25 per m³ depending on supplier and region.
Is C20 concrete strong enough for a driveway?
For a domestic driveway carrying passenger cars, C25/30 is the correct minimum, not C20. C20/25 has lower abrasion resistance and is more susceptible to surface scaling under freeze-thaw and deicing salts. Most UK contractors pour domestic driveways in C25/30 or C28/35. If the driveway carries HGVs or regular delivery vehicles, C30/37 is appropriate and the slab thickness should increase to at least 150 mm / 6 in.
How do I convert C-grade to PSI for US specifications?
Multiply the cylinder MPa by 145 to get PSI. C25 = 25 × 145 = 3,625 PSI, which rounds to 3,500 PSI in US specification. C30 = 4,350 PSI ≈ 4,000 PSI. Use the concrete PSI to MPa converter for exact two-way conversion. Note that the UK cube-strength number in the C(cylinder)/cube designation should not be used for this conversion — always use the cylinder figure.
What concrete grade do I need for a retaining wall?
For a domestic retaining wall up to 1.0 m / 3.3 ft in retained height, C25/30 is the structural minimum. For walls between 1.0–2.0 m / 3.3–6.6 ft, C30/37 with full engineering design is standard. Walls above 2.0 m / 6.6 ft retain enough lateral load that exposure class (often XC4 or XD1 in most climates) becomes the governing criterion and pushes the grade to C30/37 or C35/45. Waterproofing admixtures do not substitute for specifying the correct grade and cover depth.
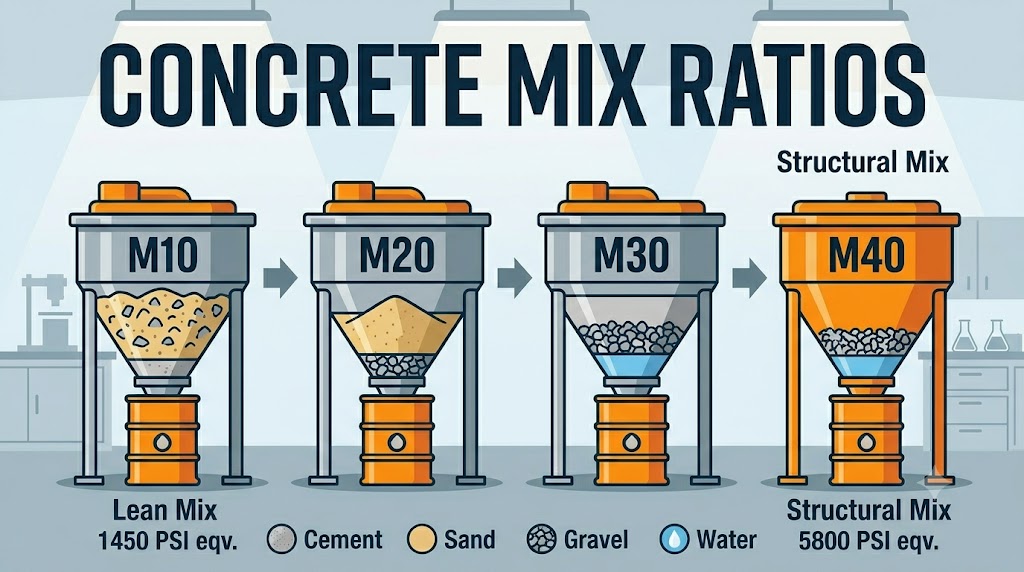
Concrete mix grades in the M-series run from M10 (roughly 1450 PSI / 10 MPa) to M40 (5800 PSI / 40 MPa) and beyond. Each grade specifies a characteristic compressive strength at 28 days and a corresponding cement:sand:aggregate ratio. Choose the wrong grade and your structure either fails under load or wastes money on over-engineered concrete.
The M-number is MPa, measured on a cube at 28 days — M20 means 20 MPa characteristic strength.
M10–M20 use fixed nominal ratios; M25 and above require a lab-designed mix, not a fixed volumetric ratio.
C-grades (UK/Australia) are cylinder strengths, not cube strengths — C25 and M25 are not the same number in practice.
The characteristic strength is a 95th-percentile floor, not the average you should mix to — target mean strength is always higher.
How mix ratios work — and what the M-number actually means
The M in M10, M20, M30 stands for mix. The number is the characteristic compressive strength in MPa (megapascals) measured on a 150 mm cube sample at 28 days. M20 = 20 MPa, which is the minimum grade permitted by most codes for reinforced concrete structural members. Picking a grade should start from the actual load the element carries, not the other way around — the Concrete Load Capacity Calculator is a useful sanity check before you commit to a grade for a beam, column, or slab.
The nominal mix ratio is expressed as cement : fine aggregate (sand) : coarse aggregate by volume. For M20 the nominal mix is 1:1.5:3, meaning 1 part cement, 1.5 parts sand, 3 parts aggregate. As grade increases, the cement content rises relative to aggregate, which increases strength and cost simultaneously.
Use the Concrete Mix Ratio Calculator to convert any M-grade into actual batch weights per cubic metre or cubic yard — accounting for the specific gravities of your materials.
M10 to M40 mix ratios, PSI equivalents, and typical applications
Grade
Ratio (C:S:A)
MPa
PSI (approx.)
Typical use
M10
1 : 3 : 6
10
1,450
Lean concrete, blinding, mass fill
M15
1 : 2 : 4
15
2,175
Plain footings, non-structural slabs
M20
1 : 1.5 : 3
20
2,900
Residential RCC slabs, beams, columns
M25
1 : 1 : 2
25
3,625
Heavy slabs, commercial foundations
M30
Design mix
30
4,350
Bridges, water-retaining structures
M35
Design mix
35
5,075
Prestressed members, marine structures
M40
Design mix
40
5,800
High-rise columns, pre-cast elements
Grades M10 to M20 use nominal mixes — fixed volumetric ratios that provide adequate strength for most residential work. M25 and above technically require design mixes, where the w/c ratio, aggregate grading, and admixture dosage are calculated from trial batches to hit a target mean strength that accounts for statistical variability. Where the table shows reinforced members (beams, columns), remember the grade only covers the concrete — the Rebar / Reinforcing Steel Calculator covers the separate reinforcement schedule those members also need.
PSI vs MPa: converting between systems
1 MPa = 145.04 PSI. To convert MPa to PSI, multiply by 145. To go the other way, divide PSI by 145. In US construction, 3,000 PSI (≈ 20.7 MPa) is the standard residential concrete specification — directly equivalent to M20. 4,000 PSI (≈ 27.6 MPa) maps closely to M25–M30. The Concrete PSI to MPa Converter handles both directions instantly, and if you’re comparing an actual core or cylinder test report against a spec, the Concrete Compressive Strength Converter covers PSI, MPa, and N/mm² together.
UK and Australian standards use C-grades (C20, C25, C30 etc.) which express the characteristic cylinder strength in MPa — the cylinder test gives results roughly 80% of the cube test, so a C25 cylinder result corresponds to a cube strength of about 31 MPa (25 ÷ 0.8), closer to M30–M31 than to a direct M25 match. Do not treat C-grades and M-grades as interchangeable without checking which test method the specification references.
Common mistakes when specifying or batching mix ratios
Using nominal ratios above M25. M30 to M40 concrete cannot reliably achieve target strength through fixed volumetric ratios. The cement content needs to be determined from water-cement ratio calculations and material-specific trial mixes — the Water-Cement Ratio Calculator is the starting point for that. Using 1:0.75:1.5 as a ‘nominal M30’ is likely to undershoot or overshoot depending on aggregate moisture and grading.
Not adjusting for aggregate moisture. Aggregate stockpiles typically carry 2–6% free moisture. If you add design water without subtracting moisture already present in the aggregate, you raise the effective w/c ratio and reduce strength — often by one full M-grade. Weigh wet and dry samples to determine free moisture before batching.
Confusing M-grade with 28-day mean strength. The M-number is the characteristic strength, meaning 95% of test samples should meet it. The target mean strength used in mix design is typically M + 1.65σ, where σ is standard deviation. For M20 with a 4 MPa SD, target mean strength is 20 + 6.6 = 26.6 MPa. Mixing to exactly M20 will fail about 50% of tests.
Using dry-volume ratios for bagging calculations. The dry ingredients occupy roughly 30–35% more volume than the finished concrete due to compaction. 1 m³ of M20 concrete requires approximately 1.54 m³ of dry mix. Ignoring the bulking factor leads to under-ordering materials by a third — pair that dry-volume adjustment with your normal project contingency using the Concrete Waste Factor Calculator so the final order accounts for both.
Related calculators you might need
Once you have your mix grade, the next step is quantifying materials. The Cement Quantity Calculator outputs bags of cement per m³ for any M-grade. If you are batching on site rather than ordering ready-mix, the Concrete Batch Calculator converts your mix design into exact weights per batch. For the water side of the equation, the Water-Cement Ratio Calculator lets you determine the precise w/c ratio for your target strength. If you are adding plasticisers or retarders to extend workability at higher grades, the Concrete Admixture Dosage Calculator converts manufacturer-recommended percentages into actual dosing volumes per m³. And once grade is settled, the Concrete Cost Calculator prices the job out at that grade.
Frequently asked questions
What is the difference between M20 and 3000 PSI concrete?
M20 has a characteristic compressive strength of 20 MPa, which equals 2,900 PSI. US residential specs typically call for 3,000 PSI (20.7 MPa). The difference is less than 4% and falls within normal test variability — for practical purposes they are the same grade. If a US specification calls for 3,000 PSI and you are sourcing locally specified M20 mix, verify with your engineer that the characteristic strength approach aligns with the project’s acceptance criteria.
What mix ratio should I use for a driveway?
A residential driveway requires a minimum of M25 / 3,500 PSI — M20 is marginal for vehicle loads and will surface-scale faster under freeze-thaw. The ratio for M25 is approximately 1:1:2 (cement:sand:aggregate) as a nominal mix. Air entrainment is essential in freeze-thaw climates — use the Concrete Air Entrainment Calculator to get the right air content dosage for your exposure. Pair the grade with an appropriate slab thickness using the Concrete Slab Thickness Selector, then use the Concrete Mix Ratio Calculator to get precise batch weights for your site.
Can I use M10 for a concrete slab?
M10 (10 MPa / 1,450 PSI) is suitable only for blinding layers and non-structural mass fill. It should not be used for any slab that carries foot traffic, furniture, vehicles, or structural loads. For a basic residential floor slab, the minimum is M20; for garage slabs or any slab carrying vehicles, M25 is the appropriate starting point. The Concrete Slab Thickness Selector pairs the grade with the right depth for the intended load.
What does ‘design mix’ mean for M30 and above?
A design mix is produced through laboratory trial batches that account for the specific gravity, absorption, and grading of your local aggregates, the cement brand’s actual strength contribution, and the required workability. Rather than a fixed ratio, a design mix specifies a maximum water-cement ratio, a minimum cement content per m³, and a target slump. Ready-mix plants supply design mixes as standard; on-site batching at M30+ requires mix design documentation from a materials lab.
How much does mix grade affect cost?
Each grade increase from M20 to M25 typically adds 8–12% to material cost due to higher cement content. M30 costs roughly 20–25% more per m³ than M20. Labour and delivery costs are unaffected by grade. The largest cost driver above M30 is usually the requirement for admixtures — superplasticisers to maintain workability at low w/c ratios add £5–£15 / $8–$20 per m³ depending on dosage rate. The Concrete Cost Per Square Foot Calculator lets you compare the installed cost across grades for a specific slab or driveway size.
Is M25 the same as C25?
No. M25 specifies a 25 MPa characteristic strength on a 150 mm cube. C25 specifies a 25 MPa characteristic strength on a 150 mm cylinder. Cylinder strengths run approximately 80% of cube strengths, so C25 ≈ M31 in equivalent cube strength terms. UK structural drawings specify C-grades; Indian and many Asian standards use M-grades. Always confirm which test geometry the project specification references before sourcing concrete.
Mix grade selection above reflects common code conventions for general planning. The correct grade for a specific structural element — and whether a nominal or design mix is acceptable — should be confirmed against your project’s structural drawings or with a qualified engineer before ordering.
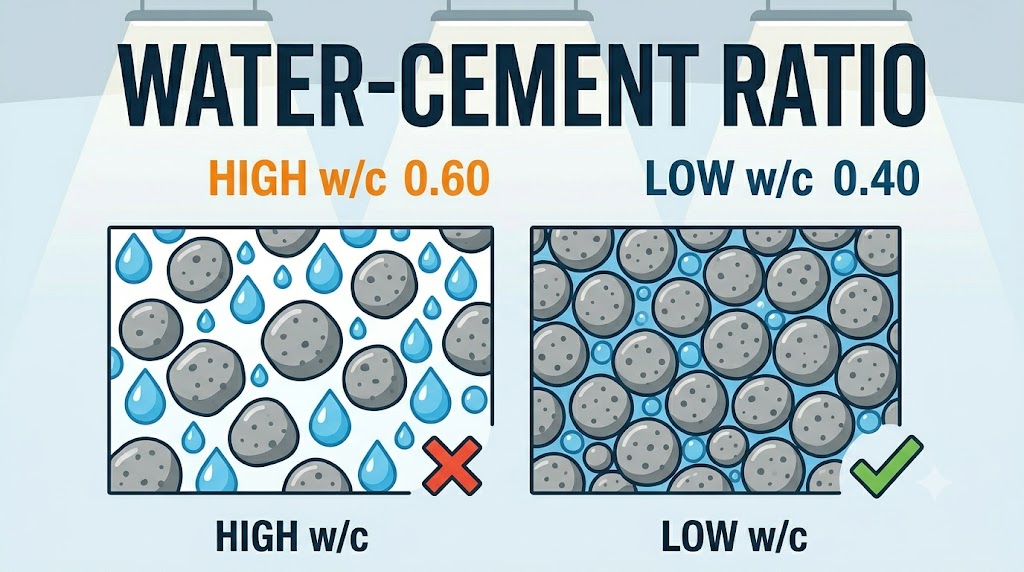
The water-cement (w/c) ratio is the weight of water in a concrete mix divided by the weight of cement. A mix with 160 kg of water and 320 kg of cement has a w/c ratio of 0.50. That one number controls strength and durability more than any other single variable: going by the ACI 211.1 mix design tables, moving from 0.40 to 0.60 costs roughly 40% of the 28-day compressive strength, and the extra water leaves the concrete more porous for the rest of its life.
Key points at a glance
Formula: w/c = weight of water ÷ weight of cement, both in the same unit.
Lower w/c means stronger, less permeable concrete, as long as the mix can still be fully compacted.
0.45–0.50 is the usual target for reinforced residential and light commercial work; codes cap it at 0.40–0.45 where deicers, seawater or sulfates are present.
Every 10 L of water added per m³ (about 2 US gal per yd³) raises w/c by around 0.03 and costs roughly 2–3 MPa / 300–450 psi.
Fix workability with admixtures, not water. A water reducer raises slump without touching the ratio.
The ratio is always by weight, never by volume. Water makes the conversion easy: 1 litre weighs 1 kg, and 1 US gallon weighs 8.34 lb.
Metric example: 175 L of water and 350 kg of cement per m³ gives 175 ÷ 350 = 0.50.
US example: 33.6 gal of water (280 lb) and 560 lb of cement per yd³ gives 280 ÷ 560 = 0.50.
One detail trips people up. The water that counts is the free water: what you add at the mixer plus any surface moisture already on the sand and stone. Water soaked up inside the aggregate particles does not count. Damp sand can carry a surprising amount, which is covered under common mistakes below.
The Water-Cement Ratio Calculator does the arithmetic in kg, lb, litres or gallons, gives an estimated 28-day strength, and checks the result against the ACI 318 exposure class you choose.
If you are site-mixing from cement, sand and stone, the ratio converts directly into water per bag:
W/C ratio
Water per 50 kg bag
Water per 94 lb sack
0.40
20.0 L
4.5 US gal
0.45
22.5 L
5.1 US gal
0.50
25.0 L
5.6 US gal
0.55
27.5 L
6.2 US gal
0.60
30.0 L
6.8 US gal
Total free water per bag of cement, including moisture already in the sand. With damp sand, add less.
This table is for plain cement. Pre-blended bagged concrete mix already contains sand and stone, so follow the water quantity printed on the bag. Our guide to bags vs ready-mix concrete explains the difference.
How the water-cement ratio determines strength
The link between water and strength was set out by Duff Abrams in 1918 and is still called Abrams’ Law: for given materials, age and curing, the strength of fully compacted concrete depends on the water-cement ratio. In formula form:
f’c = A ÷ B(w/c)
A and B are constants fitted to test results for a particular cement and aggregate, which is why the law gives the shape of the curve and trial mixes give the actual numbers.
The physical reason is simple. Cement needs only a limited amount of water to hydrate. Everything beyond that is there to make the mix workable, and when it eventually dries out it leaves a network of fine capillary pores behind. More water means more pores, and pores carry no load and let water, chlorides and sulfates in. The same excess water also rises to the surface as bleed water, leaving the top layer weakest of all.
28-day strength
W/C without air
W/C with entrained air
7,000 psi / 48 MPa
0.33
not listed
6,000 psi / 41 MPa
0.41
0.32
5,000 psi / 34 MPa
0.48
0.40
4,000 psi / 28 MPa
0.57
0.48
3,000 psi / 21 MPa
0.68
0.59
2,000 psi / 14 MPa
0.82
0.74
Approximate relationship between w/c ratio and 28-day cylinder strength for non-air-entrained and air-entrained concrete, from the ACI 211.1 mix proportioning tables.
Cutting w/c from 0.60 to 0.45 raises strength by about 45%, from roughly 26 MPa to 37 MPa (3,700 to 5,400 psi).
Cutting it from 0.60 to 0.40 raises strength by about 65%, to roughly 42 MPa / 6,100 psi.
Each 0.05 step is worth about 3–5 MPa / 450–700 psi, with the bigger gains at the low end of the range.
Entrained air costs strength: an air-entrained mix needs a w/c about 0.08–0.09 lower to reach the same figure.
Treat these as planning values. Cement type, aggregate, admixtures and above all curing shift the real result, so structural mixes are confirmed by trial batches and cylinder or cube tests. For the proportions that go with each ratio, see concrete mix ratios from M10 to M40.
W/C ratio limits by strength class and exposure
Design codes do not pick a w/c ratio for strength alone. They cap it according to what the concrete will be exposed to, because permeability, not strength, decides how long reinforcement stays protected. The three most widely used systems are below. They use different class names but land in the same place: around 0.50 for ordinary weather-exposed work and 0.40–0.45 once chlorides or severe sulfates are involved.
ACI 318 (United States and many other countries)
Class and exposure
Max w/cm
Min strength (f’c)
F1: freezing and thawing, limited exposure to water
0.55
3,500 psi / 24 MPa
F2: freezing and thawing, frequent exposure to water
0.45
4,500 psi / 31 MPa
F3: freezing and thawing, frequent water plus deicing chemicals
0.40
5,000 psi / 35 MPa
S1: moderate sulfate exposure, including seawater
0.50
4,000 psi / 28 MPa
S2: severe sulfate exposure
0.45
4,500 psi / 31 MPa
W2: in contact with water, low permeability required
0.50
4,000 psi / 28 MPa
C2: moisture plus external chlorides (deicing salts, seawater, spray)
0.40
5,000 psi / 35 MPa
Selected limits from ACI 318-19 Table 19.3.2.1. Classes F0, S0, W0, W1, C0 and C1 carry no w/cm limit. The F classes also require air entrainment.
Reinforced concrete limits from IS 456:2000 Table 5. The code also caps cement content at 450 kg/m³.
EN 206 (Europe and the UK)
Class and exposure
Max w/c
Min strength class and cement
XC1: dry or permanently wet, such as indoors
0.65
C20/25 260 kg/m³
XC2: wet, rarely dry, such as foundations
0.60
C25/30 280 kg/m³
XC3: moderate humidity, sheltered from rain
0.55
C30/37 280 kg/m³
XC4: cyclic wet and dry, exposed to rain
0.50
C30/37 300 kg/m³
XS1: airborne sea salt
0.50
C30/37 300 kg/m³
XS2: permanently submerged in seawater
0.45
C35/45 320 kg/m³
XS3: tidal, splash and spray zones
0.45
C35/45 340 kg/m³
XD3: cyclic wet and dry with deicing salts
0.45
C35/45 320 kg/m³
XF4: freeze-thaw with deicers, high saturation
0.45
C30/37 340 kg/m³ plus 4% air
Selected recommended values from EN 206 Table F.1. National provisions such as BS 8500 in the UK set the binding figures and often differ.
A warning on comparing grades across codes. Indian M grades and the second number in a European class are cube strengths. ACI’s f’c is a cylinder strength, which runs about 20% lower for the same concrete. So M25 is not 3,625 psi in ACI terms: it corresponds to C20/25, roughly 20 MPa / 2,900 psi on a cylinder. The concrete grades guide lines the systems up side by side, and the PSI to MPa converter handles the unit conversion.
Why IS 456 and EN 206 also set a minimum cement content. A low ratio only works if there is enough cement paste to coat the aggregate and fill the gaps between particles. At w/c 0.40 with 360 kg/m³ of cement, the mix holds just 144 L of water per m³ (38 US gal). A normal-slump mix without admixtures wants roughly 180–200 L, so that concrete can only be placed with a superplasticiser.
The workability problem: why contractors add too much water
Water is the cheapest and fastest way to make stiff concrete flow, which is why it gets added at the truck. The rule of thumb from the National Ready Mixed Concrete Association is that about 5 L per m³ (1 US gal per yd³) raises slump by 25 mm (1 in). Here is what that costs.
Per 10 L/m³ added: w/c rises by 0.03–0.04 for cement contents of 250–330 kg/m³, and strength falls by roughly 2–3 MPa / 300–450 psi.
Taking slump from 75 mm to 175 mm (3 in to 7 in) with water: about 20 L/m³. A mix with 320 kg of cement and 150 L of water goes from w/c 0.47 to 0.53, and its expected strength drops from about 36 MPa to 30 MPa (5,200 to 4,400 psi), a loss of around 14%.
A driver adding 50 L (13 gal) to a 6 m³ load: about 8 L/m³, or +0.03 on the ratio. It sounds small, but a mix designed right at its code maximum is now over it.
Strength is not the only casualty. Extra water means more bleeding, more drying shrinkage and a weaker, dustier surface, which is where many of the cracks covered in our crack repair guide begin.
What the rules allow on site
Adding water at the job is not banned outright. Under ASTM C94, the ready-mix specification, water may be added on arrival to bring the slump up, on these conditions: the specified maximum w/c ratio and maximum slump are not exceeded, no more than a small portion of the load (about 0.2 m³ / ¼ yd³) has been discharged, the drum is turned a further 30 revolutions at mixing speed, and the amount is measured and recorded on the ticket. Water beyond that needs the purchaser’s authorisation, and the purchaser then owns the consequences.
The right fix: admixtures
Water-reducing admixtures give the slump without the water. A normal water reducer (ASTM C494 Type A) cuts water demand by at least 5%; a high-range water reducer, or superplasticiser, cuts it by 12% to 30% or more. Used the other way round, they turn a stiff 0.45 mix into a flowing one with the ratio unchanged. Order the slump you need from the plant, or have the admixture added there. What concrete admixtures actually do covers the types, and the Concrete Admixture Dosage Calculator works out the dose for your batch.
W/C, w/cm and w/b: which ratio does your spec mean?
Most modern mixes replace part of the cement with supplementary cementitious materials (SCMs) such as fly ash, slag (GGBS) or silica fume. The ratio then has two versions:
w/c divides water by portland cement only.
w/cm (water-cementitious materials) or w/b (water-binder) divides water by cement plus SCMs.
Take a mix with 300 kg of cement, 100 kg of fly ash and 160 kg of water. Its w/c is 160 ÷ 300 = 0.53, but its w/cm is 160 ÷ 400 = 0.40. ACI 318 writes all its limits as w/cm, counting the full SCM weight. EN 206 is stricter about it: under its k-value concept only part of the addition counts, 40% for fly ash, so the same mix is assessed at 160 ÷ (300 + 40) = 0.47. Check which ratio your specification means before ordering, because the same mix can pass under one and fail under another.
Common mistakes involving water-cement ratio
1. Adding water to the truck at the pour. Take a cubic metre with 320 kg of cement and 150 L of water, w/c 0.47. Add 40 L on site and the total is 190 L, w/c 0.59. By the ACI 211.1 table the expected strength falls from about 36 MPa to 26 MPa (5,200 to 3,800 psi), more than a quarter gone from concrete that was ordered, paid for and ticketed at the higher grade. It sets, looks fine and fails a core test months later.
2. Ignoring the water already in the sand. Mix designs assume aggregate that is saturated inside but dry on the surface. Stockpiled sand is rarely like that, and a few percent of free surface moisture is common after rain. If a cubic metre uses 750 kg of sand carrying 4% free moisture, that is 30 L of water nobody measured. On the mix above it lifts w/c from 0.47 to 0.56 before a hose is touched. Batch plants correct for this with moisture tests (ASTM C566, or EN 1097-5, which replaced BS 812-109). On site, the practical answer is to hold back some of the water and add it only as needed.
3. Chasing a low ratio by cutting water alone. A ratio of 0.40 with only 200 kg/m³ of cement means 80 L of water per m³, which is far too dry to compact. The honeycombing that follows does more damage than a slightly higher ratio would have. A low w/c has to come with enough cement paste and a water reducer, which is why specifications pair a maximum ratio with a minimum cement content or a minimum strength.
4. Measuring water by eye. “Until it looks right” is how one batch ends up at 0.45 and the next at 0.60. Use a marked bucket and the same number of buckets every time. When scaling a mix up or down, scale cement, water and aggregate together; the Concrete Batch Calculator keeps every batch in proportion.
5. Mixing up w/c and w/cm. As shown above, the two can differ by 0.10 or more on the same mix. State which one you mean on the order.
6. Getting the ratio right and then not curing. A good ratio only delivers its strength if the concrete stays moist long enough to hydrate. Low-w/c mixes are the least forgiving, because they have little bleed water to protect the surface. See what concrete curing is and, for summer pours, pouring concrete in hot weather.
For structural concrete
The limits on this page are general code values for planning and for checking a delivery ticket. The exposure class, maximum ratio and minimum strength for a real structure come from the project specification, and the mix itself should be designed and tested by the supplier or a qualified engineer. Do not reduce a specified strength or raise a specified ratio without written approval.
Related calculators you might need
Water-Cement Ratio Calculator: w/c and w/cm from your water, cement and SCM weights, with an ACI 318 exposure check.
For reinforced slabs, beams, columns, driveways and foundations, aim for 0.45–0.50. Interior concrete that stays dry can go to 0.55. Concrete exposed to deicing salts, seawater or severe sulfates is limited to 0.40–0.45 by ACI 318, IS 456 and EN 206 alike. Below about 0.40 you will need a superplasticiser to place it.
How does water-cement ratio affect concrete strength?
Strength rises as the ratio falls. By the ACI 211.1 tables, lowering w/c from 0.60 to 0.40 lifts 28-day strength by about 65%, from roughly 26 MPa to 42 MPa (3,700 to 6,100 psi) for non-air-entrained concrete. Each 0.05 reduction adds about 3–5 MPa / 450–700 psi. Actual results depend on the cement, aggregate and curing.
What happens if water-cement ratio is too low?
Strength keeps rising, which is why high-strength concrete is made at 0.25–0.35, but the mix gets harder to handle. Three things change. First, it becomes too stiff to compact without a superplasticiser, and poorly compacted concrete loses more strength to voids than it gained from the low ratio. Second, below roughly 0.42 there is not enough water inside a sealed mix to hydrate all the cement, so the concrete dries itself internally and shrinks, which raises the risk of early cracking. Third, there is almost no bleed water, so the surface dries fast and must be cured immediately. The leftover unhydrated cement is not wasted; it acts as a dense filler.
How much water do I need for a bag of cement?
Multiply the bag weight by the ratio. At w/c 0.50, a 50 kg bag takes 25 L of water and a 94 lb sack takes 47 lb, or 5.6 US gallons. At 0.45 it is 22.5 L or 5.1 gallons. That is total water, so use less when the sand is damp. This applies to plain cement mixed with sand and stone, not to pre-blended bagged concrete.
Is the water-cement ratio by weight or by volume?
By weight. Mix proportions such as 1:2:4 are often given by volume, but the water-cement ratio in every modern code is a weight ratio. Because a litre of water weighs a kilogram, litres of water divided by kilograms of cement gives the ratio directly.
Can I calculate the w/c ratio from a ready-mix docket?
Often, yes. Divide the total water in litres by the cement content in kg: 160 L of water and 350 kg of cement gives 160 ÷ 350 = 0.46. Two cautions. Some dockets show only the water added at the plant and leave out aggregate moisture, and any water added on site should be written on the ticket and included. If the mix contains fly ash or slag, the figure that matters for the specification is usually w/cm. For a structural record, ask the plant for the full batch record or mix design sheet.
Does w/c ratio affect concrete curing time?
It changes how carefully you must cure more than how long. Low-ratio mixes gain strength earlier but are more sensitive to early drying, so curing has to start as soon as finishing allows. For duration, ACI 318 calls for at least 7 days of moist curing above 10°C / 50°F (3 days for high-early-strength concrete), and IS 456 calls for 7 days with ordinary portland cement and at least 10 days with blended cements or mineral admixtures. More detail is in how long concrete takes to cure, and the Concrete Curing Time Estimator gives a figure for your conditions.
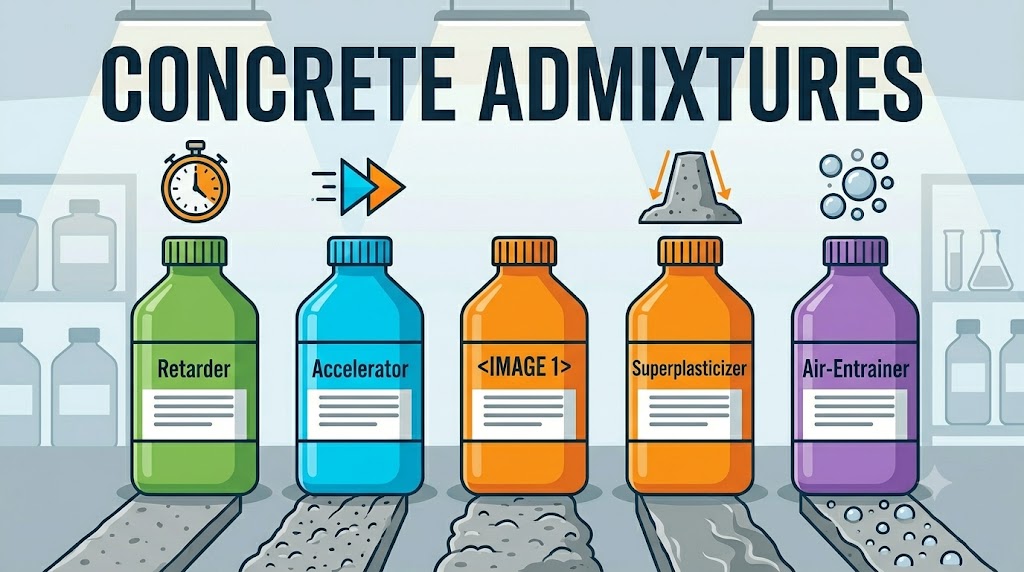
Concrete admixtures are chemical or mineral materials added to a mix — either at the plant or on site — to modify the properties of fresh or hardened concrete. The five categories used on most construction projects are water reducers, retarders, accelerators, air-entraining agents, and superplasticisers (HRWR). Each does one primary job. Using the wrong one, or using the right one at the wrong dosage, reliably causes problems.
Each admixture solves one problem — workability, set time, or durability. Using one to fix a different problem (e.g. a retarder to fix a hot-weather thermal cracking risk) doesn’t work.
Dosage is always a percentage of cement weight, same convention as pigment — never a fixed volume regardless of batch size.
Admixtures optimise a correct mix design — they don’t rescue a bad one. Wrong aggregate, wrong cement content, or no compatibility trial will still cause problems.
Never pre-blend two admixtures before dispensing — some combinations (retarder + accelerator) precipitate instantly.
The five main admixture types and their mechanism
Water reducers (plasticisers) work by dispersing cement particles through electrostatic repulsion. When cement hydrates, particles tend to flocculate — clumping together and trapping water in the floc structure. A plasticiser coats the cement surface and forces the particles apart, releasing that trapped water for workability. The result: 5–15% reduction in water demand at the same slump, or a higher slump at the same w/c ratio. This is how you improve workability without touching the water-cement ratio.
High-range water reducers (superplasticisers / HRWR) use a longer polymer chain — typically polycarboxylate ether (PCE) — that provides both steric and electrostatic dispersion. They deliver 20–40% water reduction or will fluidise a stiff mix to self-compacting concrete without affecting strength. Superplasticisers are the enabling technology for M35+ concrete: they allow low w/c ratios (0.30–0.40) to remain pourable. Dosage is typically 0.5–2.0% by weight of cement.
Retarders slow the rate of cement hydration by interfering with C3S and C3A reaction kinetics — the early-strength compounds in clinker. They extend working time from the standard 1–2 hours to 4–8 hours, or longer. Essential for hot-weather concreting above 30°C / 86°F, long-haul deliveries, large pours where all concrete must remain workable until finishing, or architectural concrete where cold joints cannot be tolerated.
Accelerators speed up cement hydration — shortening the time to initial set and accelerating early strength gain. Calcium chloride (CaCl₂) was the standard and remains permitted at low dosage in some reinforced concrete under ACI 318 (see below for the actual limits, which are more nuanced than a flat prohibition), but corrodes steel reinforcement if the dosage or exposure condition is wrong, so modern non-chloride accelerators (typically calcium nitrite or sodium thiocyanate formulations) are used instead wherever the risk isn’t worth managing. They are standard for cold-weather concreting below 5°C / 41°F, for pre-cast production where early stripping is economically important, and for repair mortars that need to carry load quickly. Cold-weather placements also need their curing schedule adjusted regardless of accelerator use — the Concrete Curing Time Estimator adjusts expected strength-gain timelines for ambient temperature.
Air-entraining agents (AEA) generate a stable network of microscopic air bubbles — 0.01–1 mm / 0.0004–0.04 in (roughly 10–1,000 microns) diameter — distributed uniformly through the paste. The bubbles act as pressure-relief chambers during freeze-thaw cycling: when pore water freezes and expands, ice crystal growth pressure is accommodated in the adjacent voids rather than cracking the paste. Correctly air-entrained concrete (4–7% air by volume, depending on aggregate size — see the dosage table below) can withstand 300+ freeze-thaw cycles without scaling; the same mix without AEA may fail in 30.
Use the Concrete Admixture Dosage Calculator to convert the manufacturer’s recommended percentage dosage into actual ml or kg per m³ for your batch volume. Manufacturer specifications are always expressed as a percentage of cement weight — so the accuracy of the dosage depends entirely on knowing your actual cement content; the Cement Quantity Calculator confirms that figure first if you’re working from a mix ratio rather than a batch ticket.
Admixture comparison: type, dosage, and when to specify
Admixture type
Typical dosage (% by cement wt)
Primary benefit
When to use
Plasticiser (WR)
0.2–0.5%
5–15% water reduction
Standard RC mixes wanting better workability without extra water
Superplasticiser (HRWR)
0.5–2.0%
20–40% water reduction
M30+, SCC, low w/c structural mixes
Retarder
0.1–0.5%
2–6 hr extended workability
Hot weather, long hauls, large monolithic pours
Accelerator (non-Cl)
1.0–3.0%
Early strength up 30–50%
Cold weather, early stripping, emergency repairs
Air-entraining agent
0.005–0.05%
4–7% air entrainment
Any exposed flatwork in freeze-thaw climates
Crystalline waterproofer
0.8–1.5%
Self-sealing capillary porosity
Water-retaining structures, basement walls
Shrinkage reducer
0.5–1.5%
Drying shrinkage down 25–50%
Industrial floors, slabs with crack sensitivity
Corrosion inhibitor
1.0–3.0%
Delays chloride attack on rebar
Marine structures, bridge decks, car parks
How admixtures interact with your mix design
Admixtures do not fix a poorly designed mix — they optimise a correctly designed one. A superplasticiser cannot compensate for aggregate that is too coarse, a cement content that is too low, or a batch that was mixed without adequate water to start. The dosage must match the cement content and type: PCE superplasticisers are sensitive to cement alkali content and C3A levels. A product that works perfectly with a CEM I 52.5R cement may be incompatible with a GGBS blend, causing flash set or loss of workability. Always request a compatibility trial from your admixture supplier before specifying a new combination.
Multiple admixtures can be combined, but must be dispensed separately into the mixer — never pre-blended together. Mixing a retarder and an accelerator in the dispenser hose will cause instant precipitation. The standard sequence is: aggregate, part water, cement, plasticiser, remaining water. Air-entraining agents are added with the initial water charge.
Dosage verification is critical. The Concrete Air Entrainment Calculator determines the AEA dosage required to hit a target air percentage based on your aggregate size and cement content — because the same dosage rate produces different air contents across different mixes. Once admixtures are in the mix, the effective w/c ratio can shift — recheck it against the Water-Cement Ratio Calculator rather than assuming the original design figure still holds.
Common mistakes when using admixtures
Adding superplasticiser directly to a stiff truck. Pouring neat HRWR onto stiff concrete at the delivery point produces an uneven dosage — some areas get the full hit of plasticiser, others get none. This creates variable workability through the load and can leave pockets of unexpectedly fluid concrete that segregate during vibration. Superplasticiser should be added at the plant with the mix water, with at least 60 seconds of high-speed mixing to achieve uniform dispersion.
Using calcium chloride accelerator without checking the applicable exposure limit. CaCl₂ is cheap and effective, but chloride ions penetrate to rebar depth and can initiate electrochemical corrosion. BS 8500 prohibits calcium chloride in all concrete containing embedded metal — a blanket rule. ACI 318 is more nuanced and sets water-soluble chloride ion limits by exposure condition: 0.06% by weight of cement for prestressed concrete (the strictest tier), 0.15% for reinforced concrete exposed to chlorides in service, 0.30% for reinforced concrete exposed to moisture without external chloride sources, and up to 1.00% for reinforced concrete that stays dry or protected from moisture in service. In practice, many specifiers avoid CaCl₂ in any reinforced element regardless of which limit technically applies, since actual service conditions can change over the structure’s life and the corrosion consequence is severe. Where the risk isn’t worth managing, use a calcium nitrite-based accelerator instead. Whatever accelerator you use, cover depth over the reinforcing steel is the other half of corrosion protection — a chloride-free mix with inadequate cover is still at risk.
Under-dosing air-entraining agent for aggregate size. The required AEA dosage increases as aggregate maximum size decreases — more surface area per unit volume means more air bubble nucleation sites are needed for the same entrained air percentage. For 20 mm / 0.75 in aggregate the target air is 4–5%; for 10 mm / 0.4 in aggregate it rises to 5–7%. Under-entraining a mix with fine aggregate will result in surface scaling after the first hard winter despite using AEA at all.
Using a retarder at elevated dosage to compensate for no cooling in hot weather. Retarders do not lower the heat of hydration — they defer it. If a mass pour in 35°C / 95°F weather is retarded to stay workable for 6 hours, the hydration heat release still occurs; it just occurs while the pour is being placed and compacted rather than afterward. Thermal cracking risk in mass pours requires pre-cooling (chilled water, ice, cooled aggregate), not retarder alone. Use both, or use a low-heat cement.
Related calculators you might need
Admixtures are one variable in a full mix design. The Concrete Mix Ratio Calculator gives you the base mix design before admixtures are specified. The Water-Cement Ratio Calculator is the critical check after a superplasticiser has reduced your water demand — verify that your effective w/c ratio is within the permitted range for your exposure class. For mixes with air entrainment, the Concrete Air Entrainment Calculator determines the specific AEA dosage for your aggregate size and target air content. If you’re batching multiple loads that all need the same dosage, the Concrete Batch Calculator keeps admixture-to-cement ratios consistent across every batch, the same way it does for pigment dosing. And if you are evaluating whether admixtures justify the cost increase over a standard mix, the Ready-Mix vs Bagged Concrete Cost Calculator gives you the overall material cost comparison for your project volume.
Frequently asked questions
What admixture should I add to concrete in hot weather?
Use a set retarder dosed at 0.2–0.4% by cement weight. For temperatures above 30°C / 86°F, a standard retarder extends workability by 2–3 hours; above 35°C / 95°F you may need a ‘hot weather’ retarder formulation that extends to 4–6 hours. Also pre-cool the mixing water — replacing part of the water with ice is simple and reduces concrete temperature by 3–5°C / 5–9°F per 10% replacement. Do not add extra water to compensate for stiffening.
What does a plasticiser do that adding more water doesn’t?
Both improve workability, but adding water raises the w/c ratio and permanently reduces strength and durability. A plasticiser at 0.3% cement weight achieves the same slump increase as adding 12–15 litres / 3–4 US gallons per m³ of water, with no effect on w/c ratio or 28-day strength. The cost of a plasticiser dose is typically £1–£3 / $1.50–$4 per m³ — less than the material cost of the strength loss you would incur by adding water instead.
Can I use admixtures in bagged concrete mixed on site?
Yes — liquid admixtures are simply added to the mixing water before it contacts the cement. Measure the cement weight of your batch (a 25 kg / 55 lb bag weighs 25 kg), calculate the admixture dosage as a percentage of that weight, then add that mass or volume of admixture to your measured water. For a 25 kg cement bag, a 0.3% plasticiser dosage is 75 ml (about 5 tablespoons). A pipette or measuring syringe gives acceptable accuracy for on-site use. If you’re mixing several bags across a pour, the Concrete Batch Calculator scales the dosage proportionally so every batch matches.
Are admixtures safe to handle?
Most liquid plasticisers and retarders are low-hazard — they are aqueous solutions with pH 5–9 and present no significant inhalation or ingestion risk at normal dosage handling. Air-entraining agents contain surfactants that can irritate eyes and skin on contact; wear gloves and eye protection when handling neat liquid. Calcium chloride accelerator (where still used) is corrosive at concentrations above 30%. Always read the product SDS before use, and keep admixtures away from rebar stockpiles to prevent chloride contamination.
How do I know if my concrete has enough air entrainment?
The only reliable on-site check is a pressure air meter test (ASTM C231 / BS EN 12350-7) performed on fresh concrete from the truck immediately before or during the pour. Target air content for freeze-thaw exposure is 4–7% depending on aggregate size. A visual inspection tells you nothing — the bubbles are microscopic. Specify that the driver carries a docket showing the AEA dosage used, and require fresh-concrete air testing on any pour of 5 m³ / 6.5 yd³ or more in exposed locations.
Dosage figures above are general working ranges for planning. Always confirm the recommended dosage against the specific product’s data sheet, run a compatibility trial with your actual cement source before a structural pour, and confirm chloride and exposure-class limits with your project specification or a qualified engineer — this is especially important for accelerators, corrosion inhibitors, and any reinforced element.
Air entrainment is mandatory for any concrete that will experience freeze-thaw cycling. Without it, water in the concrete expands when it freezes, generating internal hydraulic pressure that exceeds the tensile strength of the paste and causes progressive surface scaling and spalling. A single winter season is enough to begin visible damage on non-air-entrained flatwork in a climate that cycles between freezing and thawing — which covers most of the northern US, Canada, the UK, northern Europe, and elevated regions of Australia.
How air entrainment works and what the target air content should be
Air-entraining admixtures — typically vinsol resin, tall-oil derivatives, or synthetic surfactants — reduce the surface tension of water during mixing, causing billions of microscopic air bubbles (typically 10–300 µm diameter) to form and stabilise within the cement paste. These bubbles are not the same as entrapped air (the large, irregular voids from poor consolidation). Entrained air bubbles are small, uniformly distributed, and deliberately engineered.
When water in the concrete freezes and expands (water expands roughly 9% by volume on freezing), the entrained air voids act as pressure relief chambers. The expanding ice has somewhere to go. Without those voids, the hydraulic pressure builds until the paste cracks. The mechanism requires the bubbles to be close enough together — the spacing factor between adjacent air voids should be no more than 0.2 mm (0.008 inches) per ACI 318 and ACI 201.2R. This is a function of the total air content and bubble size distribution, not just air percentage alone.
Use the concrete air entrainment calculator to determine required admixture dosage based on your aggregate size, target air content, and concrete volume. Dosage is sensitive to mix design and ambient temperature — the calculator adjusts for these variables.
Target total air content by aggregate size, per ACI 318 Table 19.3.3.1:
Nominal max aggregate size
Mild exposure
Moderate exposure
Severe exposure
9.5 mm (3/8 in)
4.5%
6.0%
7.5%
12.5 mm (1/2 in)
4.0%
5.5%
7.0%
19 mm (3/4 in)
3.5%
5.0%
6.0%
25 mm (1 in)
3.0%
4.5%
6.0%
37.5 mm (1.5 in)
2.5%
4.5%
5.5%
Severe exposure: concrete exposed to freeze-thaw cycles in a moist condition and to deicing salts. Moderate: freeze-thaw cycles without deicing chemicals. Mild: occasional freezing with low saturation. In the UK and Ireland, BS 8500-1 uses equivalent exposure classes (XF1–XF4), with XF4 (road and bridge decks with de-icing salts) requiring 4–7% total air.
Where air entrainment is actually required — and where it is not
Required: Any outdoor flatwork in a freeze-thaw climate — driveways, footpaths, patios, parking areas, pool decks, exposed slabs. Any structural element in a freeze-thaw climate that is in a moist or saturated state: retaining walls, foundations at or above grade, bridge decks, pavements. Concrete exposed to deicing salts needs both air entrainment and a low water-cement ratio (0.40 or below per ACI 318 for severe exposure).
Not required: Interior slabs (garage floors with no external freeze exposure, warehouse floors, basement slabs). Concrete in permanently dry conditions. Concrete in warm climates where air temperature never drops below 0°C / 32°F with the concrete in a saturated state. Mass concrete where thermal mass prevents freeze-thaw cycling.
Air entrainment is also used — separately from freeze-thaw protection — to improve workability in low-slump mixes. Each 1% of entrained air reduces water demand by approximately 3–5 litres per m³ (0.5–0.9 gal/yd³), which can partially offset the water-cement ratio without reducing workability. This application is less common but relevant in stiff paving mixes.
Common mistakes
Specifying air entrainment in interior slabs. Air-entrained concrete used for interior floor slabs that will receive a hard-trowel finish is a significant mistake. The entrained air voids open at the surface during troweling if finishing happens too early or too aggressively, leaving a pitted, weak surface layer. Interior concrete on grade does not experience freeze-thaw cycling — the freeze-thaw protection is irrelevant, and the surface quality penalty is real. Specify non-air-entrained concrete for interior slabs, regardless of what the ready-mix plant offers as a default.
Not testing air content on site before placement. Air content in the delivered concrete can differ from the batch plant target due to temperature changes in transit, variation in admixture dosage, or aggregate moisture. The only way to know what you are placing is to test it. ASTM C231 (pressure meter method) and ASTM C173 (volumetric method, for lightweight or slag aggregates) both take under five minutes. Accepting a truckload without testing the air content is standard practice in residential work — and the reason many residential driveways fail within three winters.
Finishing air-entrained concrete too early. Troweling before bleed water has fully evaporated seals the surface and traps moisture below, which later forms a weak delamination layer. The correct trigger for finishing is when the bleed water sheen disappears and the surface can support the finisher’s weight without significant indentation — typically 1–3 hours depending on temperature and relative humidity. Premature finishing is responsible for the majority of surface scaling complaints on air-entrained flatwork.
Assuming higher air content is always better. Air content above the ACI maximum for a given aggregate size begins to reduce compressive strength significantly — roughly 5% strength reduction per 1% increase in total air content. An over-entrained mix at 9–10% total air on a 19 mm aggregate may meet the durability goal but drop compressive strength by 15–20% relative to the designed mix. If you need both freeze-thaw durability and high strength (for example, a driveway subject to deicing salts), the solution is the correct air content range plus a low water-cement ratio, not excess air.
Related calculators you might need
Air entrainment works best when the rest of the mix design is also dialled in. The water-cement ratio calculator is particularly important here: ACI 318 requires a maximum w/c of 0.40 for concrete exposed to deicing chemicals and freeze-thaw in a moist condition. If you are adding an air-entraining admixture alongside other chemical admixtures (a water reducer, for instance), the concrete admixture dosage calculator helps you calculate combined dosages and check compatibility. For driveways and patios specifically, the concrete driveway calculator and concrete patio calculator give you the volume to order — take that figure to the batch plant along with your specified air content range. Once the slab is placed and cured, the concrete sealer coverage calculator sizes the penetrating sealer needed to extend service life further.
Frequently asked questions
Does all concrete in cold climates need air entrainment?
Only concrete that will be in a moist or saturated condition when freezing temperatures arrive. A concrete foundation below a heated building, for instance, may not be subject to freeze-thaw cycling even in a cold climate. The critical combination is: concrete that is wet (above roughly 80% internal relative humidity) AND subject to temperatures cycling below 0°C / 32°F. Outdoor flatwork in any northern US state, Canadian province, or most of northern and central Europe meets both conditions by default. Specify air entrainment for all exposed outdoor concrete in these regions without exception.
What happens if air content is too low or too high?
Too low (below the minimum target range): freeze-thaw damage begins within 1–3 seasons in cold climates. Surface scaling appears first — a characteristic flaking of the top 1–3 mm of paste — followed by progressive aggregate exposure and structural deterioration. Too high (above the maximum target range): compressive strength drops and surface finishability suffers. At 2–3% above the maximum ACI target, strength reduction is meaningful (10–15% on some mix designs). The target range is a range for a reason — aim for the midpoint at the batch plant.
Can I add air-entraining admixture to a bagged concrete mix?
Yes, but it requires careful dosing. Standard bagged concrete mixes (Quikrete 5000, Sakrete, etc.) do not contain air-entraining admixture. You can add a liquid air-entraining admixture to the mix water at the manufacturer’s recommended dosage per bag. The challenge is that hand-mixing produces inconsistent air distribution — a drum mixer gives better results. You will not be able to verify air content without a pressure meter, so testing is impractical for small site mixes. For a driveway, walkway, or patio in a freeze-thaw climate, ready-mix concrete with specified and tested air content is a considerably more reliable option than trying to air-entrain bagged concrete on site.
How do I know if my ready-mix supplier is delivering the right air content?
Ask for the batch ticket with every load and check that the air-entraining admixture dosage is consistent with what you specified. More importantly, perform an on-site air content test using a Type B pressure meter (ASTM C231) on the first truck of every pour. Target your specified range — typically 5.5–7.5% for a residential driveway in a severe exposure climate. If the test comes in below 4.5% or above 8.5% on standard aggregate, reject or hold the load and call the plant to adjust before pouring.
Does air entrainment affect concrete colour or appearance?
Air-entrained concrete is slightly lighter in colour when fresh compared to non-air-entrained concrete of the same mix design — the additional voids reduce the density of the paste. After curing and sealing, the colour difference is minimal for most standard grey or pigmented mixes. The more relevant appearance issue is surface texture: correctly finished air-entrained concrete looks the same as non-air-entrained concrete. Incorrectly finished concrete (troweled too early or too aggressively) will show a pitted surface from air voids opening at the paste surface.
Can air entrainment fix concrete that was not air-entrained at placement?
No. Air entrainment is a mix design decision made at the batch plant. Once concrete is placed and hardened, there is no way to add or improve freeze-thaw durability through surface treatments alone. Penetrating sealers reduce surface water absorption and extend the service life of non-air-entrained flatwork in mild exposure conditions, but they are not a substitute for entrained air in a severe freeze-thaw environment. If a driveway or patio was placed without air entrainment in a climate where it was required, the realistic outcome is resurfacing (see the concrete resurfacing calculator for material quantities) or full replacement within 5–10 years.
Concrete pigment is dosed as a percentage of the cement weight, not of the concrete volume. Most integral colours fall between 1% and 6% of cement weight, colour stops deepening at around 5–6%, and ASTM C979 caps the dose at 10%. So a mix with 350 kg of cement per m³ coloured at 5% needs 350 × 0.05 = 17.5 kg of pigment per m³ (about 30 lb per yd³).
Key points at a glance
Formula: pigment weight = cement weight × dosage %. Fly ash and slag count as cement for this purpose.
Working range: 1–6% for most iron oxide colours. Beyond about 6% you pay for pigment that adds almost no colour.
Hard limit: 10% of cement weight under ASTM C979.
Always weigh, never scoop. Pigment powders vary too much in density for volume measures to repeat.
Water changes colour as much as pigment does. A wetter batch cures paler, so keep the water identical from batch to batch.
Metric: 350 kg of cement per m³ at 5% = 17.5 kg of pigment per m³.
US: a 6-sack mix has 564 lb of cement per yd³. At 5% that is 28 lb of pigment per yd³.
US colour charts quote the dose as pounds of pigment per 94 lb sack of cement. Because a sack is close to 100 lb, the two systems nearly match: 2 lb per sack is roughly 2%, 5 lb per sack roughly 5%.
If the mix contains fly ash or slag, base the dose on the total cementitious weight, cement plus those additions. Pigment makers specify it that way because the pigment tints the whole paste, not only the portland cement.
On cost: at an assumed retail price of $3.50–$6.00 per kg ($1.60–$2.70 per lb) for iron oxide, the 17.5 kg in the metric example adds roughly $60–$105 per m³. Pigment prices vary widely by colour and pack size, so check your supplier’s current figure.
If you know your mix ratio but not the cement weight, the Concrete Mix Ratio Calculator or the Cement Quantity Calculator gets you that number first. Then the Concrete Pigment and Color Calculator takes your concrete volume, cement content and a colour intensity from light (1.5%) to maximum (7%), and returns the total pigment, the number of pigment bags to buy and the material cost.
0.25–1.0 kg per 50 kg bag 0.5–1.9 lb per 94 lb sack
Medium
2–4%
1.0–2.0 kg per 50 kg bag 1.9–3.8 lb per 94 lb sack
Dark, near saturation
4–6%
2.0–3.0 kg per 50 kg bag 3.8–5.6 lb per 94 lb sack
ASTM C979 maximum
10%
5.0 kg per 50 kg bag 9.4 lb per 94 lb sack
General ranges for iron oxide pigments on grey cement. The dose for a named colour comes from the manufacturer’s colour chart.
How much pigment per bag of concrete mix?
Pre-blended bagged concrete is mostly sand and stone, and the cement content is not printed on the bag. As a working estimate, cement makes up roughly 12–15% of the bag, so an 80 lb (36 kg) bag holds about 10–12 lb (4.5–5.5 kg) of cement.
At 5%: about 0.5–0.6 lb (225–270 g) of pigment per 80 lb bag, or 5–6 lb (2.3–2.7 kg) across a 10-bag pour.
Retail colour packs: many are sold as “1 lb per bag”. On an 80 lb bag that works out to roughly 8–10% of the cement, which is the strongest shade the product is meant to give. For a lighter colour, use part of the pack and weigh it.
Where the pigment maker prints a per-bag rate, follow it; they have tested it with typical bagged mixes. The Concrete Bags Calculator gives you the bag count so the pigment order scales with it.
Why dosage percentage matters: the chemistry behind colour saturation
Concrete pigments are fine, insoluble mineral particles, not dyes. They are roughly one-tenth the size of cement grains, so they disperse through the cement paste and tint it, and the tinted paste then coats every grain of sand and stone. That is why the dose follows the cement: more paste needs more pigment to reach the same colour, while extra aggregate needs none.
Three things happen as the dose rises:
Below about 1%, the grey of the cement dominates. You get a tint, not a colour.
From about 1% to 5%, colour deepens steadily with each addition.
At around 5–6%, good-quality pigments reach saturation. The paste is as coloured as it can get, and more pigment mostly adds cost.
High doses also affect the concrete itself. Pigment is an extra load of very fine powder, and fine powder needs water to wet it. If that water is added, the water-cement ratio rises and strength falls. ASTM C979 is written around this: at its maximum dose a compliant pigment may not push the water-cement ratio above 110% of the plain mix, drop 28-day strength below 90% of it, or change the air content by more than 1%. It may not speed up setting by more than an hour or delay it by more than an hour and a half. The European standard, EN 12878, has a separate category for pigments used in reinforced concrete, with limits on chlorides and a cap on strength loss.
In practice, that means a certified pigment at normal doses is not a strength problem, provided nobody adds water to compensate. If a heavily pigmented mix is too stiff, use a water reducer; the Concrete Admixture Dosage Calculator works out the dose.
Pigment types and what to know about each
Pigment
Colours
What to know
Iron oxide red (Fe₂O₃)
Reds, terracotta, brick
The most widely used pigment. Stable in sunlight and in the alkalinity of cement.
Iron oxide yellow (FeOOH)
Buff, tan, gold
Heat-sensitive: products are rated to about 150–175°C / 300–350°F, above which the colour shifts toward red.
Iron oxide black (Fe₃O₄)
Greys to charcoal
Becomes a permanent part of the paste. Slightly brownish next to carbon black.
Carbon black
Deep, jet black
Two to five times the tinting strength of iron oxide black, but it can leach out and fade unless kept sealed, and it can reduce entrained air.
Brown blends
Browns, umbers
Mixtures of red, yellow and black. Shade varies between suppliers, and some contain carbon black.
Chromium oxide (Cr₂O₃)
Greens
Considerably more expensive than iron oxides.
Cobalt-based
Blues
The most expensive option. Usually paired with white cement.
Titanium dioxide
White, lightening
Limited effect in grey concrete. White cement usually brightens a mix more effectively.
Dosage recommendations vary between manufacturers even within one colour family. Confirm against the data sheet for the product you have bought.
Iron oxide black or carbon black? For exterior concrete, and especially anywhere with freeze-thaw cycles, iron oxide black is the safer choice. It will not leach, and it does not interfere with the air-entraining admixture that protects the slab; see air entrainment in concrete for why that matters. Carbon black gives a deeper black for less money, which suits interior work and surfaces that will stay sealed.
Grey or white cement? Grey cement mutes every colour. The same 5% red that gives a bright terracotta on white cement gives a subdued brick-brown on grey. For pastels, clean yellows, blues and bright reds, white cement is close to essential. It costs noticeably more than grey cement, so it tends to be reserved for decorative work such as stamped slabs, exposed aggregate and countertops.
What else changes the colour besides dosage
Two pours with exactly the same pigment dose can still come out different. These are the usual reasons, in rough order of how often they cause trouble:
Water content. The most common source of colour variation. A higher water-cement ratio cures paler. Do not add water to one load and not the next, do not sprinkle the surface, and do not finish with a wet trowel or broom.
Cement and additions. Cement colour varies by brand and plant, and fly ash and slag shift it again. Keep the same cement, the same source and the same proportions for the whole job.
Finishing. A broom or light texture gives the most uniform colour. Heavy trowelling and changing tools partway through both show up as shade differences.
Curing method. Water curing, wet coverings and plastic sheeting all cause blotching on coloured concrete. Use a curing compound made for coloured concrete, applied as soon as finishing is done. Our guide to concrete curing covers the methods.
Calcium chloride. Chloride-based accelerators discolour coloured concrete. Use a non-chloride accelerator if you need one.
Time. Concrete lightens as it cures and dries. Judge the colour at about 28 days, not the morning after the pour.
Because so many variables are in play, the only reliable preview is a test panel: the same mix, the same finish, the same curing compound and sealer, made by the same crew, and left to cure before anyone approves the colour.
Mixing order: powder and liquid pigments
Powder, mixing by hand or in a small mixer: blend the pigment thoroughly with the dry materials first. Then add about two-thirds of the water, mix until the colour is even, and add the rest to reach a workable consistency.
Liquid colour: follow the product instructions, which normally have you stir it into the mixing water. The water in the colour counts as part of the mix water.
Ready-mix: give the plant the colour name or the dose and let them batch it. Many integral colours come in bags that dissolve in the drum, so the whole bag goes in unopened.
Whatever the method, do it the same way every time. For anything larger than a small slab, one ready-mix load is far easier to keep uniform than a long run of hand-mixed batches; bags vs ready-mix concrete compares the two.
Common mistakes
1. Measuring pigment by volume instead of weight. Pigment powders differ in how densely they pack, and the same powder packs differently when scooped loosely or pressed down. A cup of one colour does not weigh the same as a cup of another. Weigh every dose on a scale that reads to 10 g (¼ oz) or better.
2. Letting the cement content drift between batches. Colour depends on the ratio of pigment to cement. If one batch has 320 kg of cement and the next has 370 kg, the same 16 kg of pigment is 5.0% in the first and 4.3% in the second, and the second will be visibly lighter. The Concrete Batch Calculator keeps every batch in the same proportions.
3. Adjusting the water from batch to batch. This undoes careful weighing faster than anything else. Fix the water quantity and measure it, exactly as you do the pigment.
4. Judging the colour before the sealer goes on. Sealers change the look. A penetrating sealer leaves the surface looking much as it was, while a film-forming acrylic, especially a solvent-based one, deepens the colour and adds sheen. Approve the colour on a sample that has the sealer you intend to use. How to seal concrete explains the types, and the Concrete Sealer Coverage Calculator sizes the order.
5. Curing coloured concrete like plain concrete. Sprinklers, wet burlap and plastic sheeting are fine on a grey slab and leave blotches on a coloured one.
6. Under-ordering pigment. Running short mid-pour means a colour break at the batch line or a reorder from a different production lot that may not match. Buy all the pigment for the job at once, from one lot, with the same overage you allow for the concrete; the Concrete Waste Factor Calculator suggests a margin.
An 80 lb / 36 kg bag of premixed concrete contains roughly 10–12 lb / 4.5–5.5 kg of cement. At a 5% dose that is about 0.5–0.6 lb / 225–270 g of pigment per bag, or 5–6 lb / 2.3–2.7 kg for ten bags. Retail packs labelled “1 lb per bag” give a much stronger shade, around 8–10% of the cement. If your pigment’s data sheet gives a per-bag rate, use that.
Will adding pigment weaken my concrete?
Not noticeably at normal doses, as long as you do not add extra water. Pigments certified to ASTM C979 must keep 28-day strength at 90% or more of the plain mix even at their maximum dose, which can be no higher than 10% of cement weight. The real risk is indirect: pigment makes the mix a little stiffer, someone adds water to loosen it, and the water costs the strength. If strength matters, have the mix designed and tested with the pigment in it.
Does concrete colour fade over time?
Iron oxide pigments are lightfast and do not fade in sunlight. What changes is the surface around them: efflorescence leaves a white film that makes dark colours look washed out, wear exposes sand and stone, and dirt dulls the finish. Carbon black is the exception among pigments, because it can leach out with repeated wetting and drying. Keeping the slab sealed protects against all of these. Resealing intervals depend on the sealer, typically every 1–3 years for acrylics and 3–7 years for penetrating sealers.
Can I mix two pigment colours together?
Yes. Iron oxides are compatible with one another, and most browns and tans are blends of red, yellow and black. Blend the powders dry, record the weights of each so you can repeat it, and keep the combined dose within the 10% limit. Test the blend on a cured, sealed sample before committing, because colour shifts from wet to dry and again under a sealer.
What is the difference between liquid pigment and powder pigment for concrete?
They contain the same pigments. Liquid colour is pigment already dispersed in water, which makes it easy to meter automatically, so ready-mix plants often prefer it. Powder is more concentrated by weight and simpler to store and weigh for site mixing. A litre of liquid colour contains less pigment than a kilogram of powder, so the dose is not interchangeable: use the equivalent given on the product data sheet, and count the water in the liquid as part of the mix water.
When should I judge the final colour?
After about 28 days of curing, and with the sealer applied if you plan to use one. Fresh coloured concrete looks darker and more intense than it will once it has cured and dried, so a slab that seems too strong on day two is usually closer to the sample by the end of the month.
Pennsylvania Aggregates and Concrete Association, colored concrete practice sheet: water content, finishing and curing of coloured concrete.
Sika Scofield, integral color guide: dosage per sack of cementitious material, mock-ups and curing cautions.
Dosage figures on this page are general working ranges for planning. Always confirm the recommended dose on your pigment’s data sheet and test a sample before committing to a full pour, because colour response varies with the cement, the aggregate and the water content even at an identical dose. How we check our figures is set out in our editorial policy.
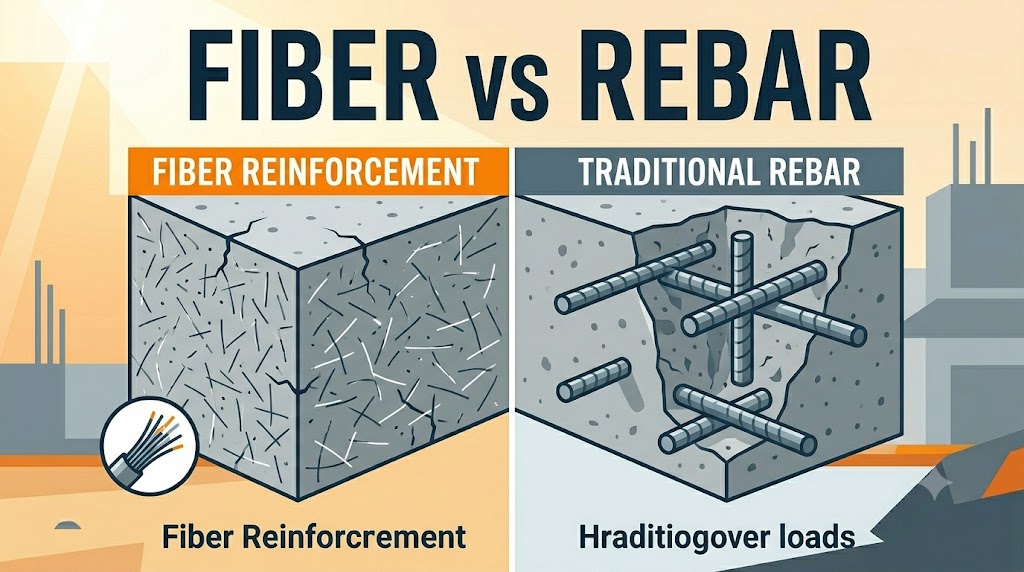
Fiber reinforcement does not replace rebar for structural applications. That is the most important thing to understand before comparing the two. Fibers control shrinkage cracking and improve toughness; rebar carries tensile load. Choosing between them — or combining them — depends entirely on what the concrete is being asked to do.
How fiber reinforcement and rebar actually work
Concrete is strong in compression and weak in tension. Rebar solves the tension problem by embedding steel bars that carry tensile forces the concrete cannot handle alone. This is structural reinforcement: it prevents failure under load and keeps a cracked section from separating. Without it, a loaded slab or beam can crack through and collapse.
Fiber reinforcement works differently. Synthetic fibers — typically polypropylene at 12–19 mm for micro-fibers, or nylon and polyester for macro-fibers — are distributed randomly throughout the mix. They do not form a continuous load path the way a rebar mat does. What they do is bridge micro-cracks as they form, limiting crack width and slowing propagation. Steel fibers (typically 30–60 mm, hooked-end) can carry meaningful post-crack load in industrial flooring, but they still cannot replicate the directional tensile capacity of a placed rebar layout in structural members.
Side-by-side comparison: cost, labour, lifespan, and use cases
This table covers the real decision variables — not theoretical ones.
Factor
Synthetic Micro-Fiber
Steel / Macro-Fiber
Rebar (mild steel)
Material cost (per m³ / yd³)
$3–$8 / $2.50–$6.50
$18–$45 / $15–$38
$20–$80+ depending on layout
Labour impact
Mixed in with batch — zero extra placement labour
Same as synthetic — no placement work
Requires cutting, bending, tying, and placement; adds 1–4 hrs per 10 m² / 110 ft²
Crack control
Controls plastic and early drying shrinkage cracks
Controls shrinkage and improves post-crack toughness
Controls structural cracks under load; minimal effect on early shrinkage
Structural capacity
None
Partial — only in certain slab-on-grade designs with engineering approval
Full — designed tensile capacity per ACI 318 / AS 3600 / BS EN 1992
Typical lifespan
Same as the concrete — 30–50+ years
Same as the concrete if corrosion-resistant type used
50–100 years with adequate cover; shorter if corrosion occurs
Best use cases
Footpaths, driveways, patios, pool decks, residential slabs
Industrial floors, warehouse slabs, precast elements
Footings, beams, columns, retaining walls, any structural element
When fiber alone is sufficient — and when it is not
Micro-synthetic fibers are sufficient for any non-structural flatwork where the primary risk is plastic shrinkage cracking: residential driveways, sidewalks, patios, shed pads, and pool decks. At a typical dosage of 0.6–0.9 kg/m³ (1.0–1.5 lb/yd³), they distribute into millions of filaments per cubic metre and intercept micro-cracks before they become visible. The concrete still cracks — all concrete cracks — but the cracks stay narrow and do not open up.
Where fiber reinforcement is not sufficient:
Any element that carries load in bending — beams, suspended slabs, lintels — needs rebar. The tensile stress at the bottom of a loaded beam cannot be resisted by randomly distributed short fibers. Any retaining wall resisting lateral earth pressure needs rebar, typically at both faces. Any footing transferring column or wall loads to soil needs rebar. Fibers in these applications are a secondary addition at best, not a substitute.
Steel fibers in industrial slab-on-grade applications are a different conversation. Dosages of 25–40 kg/m³ (42–67 lb/yd³) can replace conventional rebar mats in ground-supported floors where the primary loading is distributed (forklifts, racking loads) and joint-free slab construction is the goal. This requires a structural engineer, a fibre supplier’s design tool, and compliance with TR34 (UK/international) or ACI 360 (US).
Common mistakes
Treating micro-fibers as a one-for-one rebar substitute in structural work. This is the most dangerous misunderstanding in the comparison. A contractor who swaps out a rebar mat for a fiber dose in a footing or retaining wall has not simplified the job — they have created a structural deficiency. Micro-fibers carry zero tensile load in a cracked section under sustained stress. The correct approach: use fibers for shrinkage control and rebar for structural performance, often together.
Using rebar to solve a plastic shrinkage cracking problem. If a slab cracks within the first 24 hours — before the concrete has hardened — rebar provides no benefit. Plastic shrinkage cracking is caused by the surface drying faster than water bleeds up from below. The fix is fiber reinforcement (prevents crack initiation), windbreaks, evaporation retarder, and curing covers — not additional steel.
Inadequate rebar cover. The standard minimum cover for rebar in a slab-on-grade is 38 mm / 1.5 inches from the bottom. Contractors who place chairs incorrectly — or none at all — end up with rebar sitting at mid-depth or lower, where it contributes almost nothing to flexural capacity. Rebar at mid-slab resists neither top-fibre tension nor bottom-fibre tension effectively.
Assuming all fibers are equivalent. A 12 mm polypropylene micro-fiber added at 0.6 kg/m³ is a crack-control additive. A 50 mm hooked-end steel fiber at 35 kg/m³ is a structural material. Using the former in an industrial floor application and expecting structural-grade crack resistance is a dosage and product mismatch. Check the fiber type, length, aspect ratio, and the supplier’s dosage curves.
Related calculators you might need
If you are designing the reinforcement layout for a slab, the rebar / reinforcing steel calculator converts your bar size and spacing into total weight and linear metres — useful when comparing the steel cost against a fiber dosage. For laying out the grid itself, the rebar spacing calculator handles bar centres for a given slab thickness and load. For the concrete itself, the concrete mix ratio calculator helps you confirm that the base mix design is compatible with fiber addition (water-cement ratio and workability both affect fiber distribution). If the project involves a structural slab and you need to verify load capacity, the concrete load capacity calculator gives you a working baseline before involving a structural engineer.
Frequently asked questions
Can I add fiber to a mix that already has rebar?
Yes — combining both is standard practice in industrial slabs, driveways, and concrete structures in aggressive environments. Synthetic micro-fibers control early shrinkage cracking independently of the rebar layout. Steel fibers in structural-grade dosages can sometimes allow rebar reduction, but only with engineering sign-off. For most residential and commercial flatwork, adding 0.6–0.9 kg/m³ of polypropylene fiber to a rebar-reinforced slab is straightforward and has no negative effect on the rebar.
Is fiber reinforcement cheaper than rebar?
For the material alone, micro-synthetic fibers typically add $3–$8 per m³ ($2.50–$6.50 per yd³), which is cheaper than most rebar layouts. The real cost difference is labour: rebar requires cutting, tying, and placing, which adds meaningful time on site. For a 100 m² / 1,075 ft² driveway, rebar placement can add 6–8 hours of skilled labour. Fiber is added at the batch plant and requires nothing on site. However, if structural reinforcement is required, rebar is not optional — no labour saving justifies the omission.
What does fiber reinforcement actually do to concrete strength?
Micro-synthetic fibers at standard dosages (0.6–0.9 kg/m³) have no meaningful effect on compressive strength — typically less than 1–2 MPa difference. They improve toughness (energy absorption after cracking) and reduce plastic shrinkage crack width by 80–90% in controlled tests. Steel fibers at high dosages (30–40 kg/m³) increase post-crack flexural strength and toughness substantially, which is why they are used in industrial floor design. Neither fiber type increases the 28-day compressive strength the way an improved mix design or lower water-cement ratio would.
Does fiber reinforcement stop concrete from cracking entirely?
No. Every concrete element will crack at some point — thermal movement, drying shrinkage, and load-induced stress all exceed concrete’s tensile strength under normal service conditions. What fibers do is limit crack width and spacing. A slab with synthetic fibers at adequate dosage will still crack, but the cracks will be narrower (typically under 0.2 mm at early age) and more numerous rather than fewer wide cracks. That is the desired outcome: distributed fine cracks are structurally and aesthetically less damaging than isolated wide ones.
How do I calculate the right fiber dose for my project?
Standard residential dosage for polypropylene micro-fiber is 0.6 kg/m³ (1.0 lb/yd³) for general flatwork, and up to 0.9 kg/m³ (1.5 lb/yd³) for slabs with higher shrinkage risk (large surface area, hot weather, low humidity). Use the concrete fiber reinforcement calculator to convert your slab volume into total fiber weight by dosage rate. For steel fiber in industrial applications, use the supplier’s design guide — dosage ranges from 20 to 40 kg/m³ depending on the design method and loading scenario.
Can I use fiber reinforcement in footings?
Micro-synthetic fibers in footings control plastic shrinkage cracking during cure, which is useful in hot conditions. They do not, however, provide the tensile reinforcement that footings require. A strip footing, pad footing, or pile cap must have rebar sized and placed to an engineer’s specification. Adding fibers to a footing mix is acceptable as a secondary measure but does not reduce or eliminate the rebar requirement under any major building code.